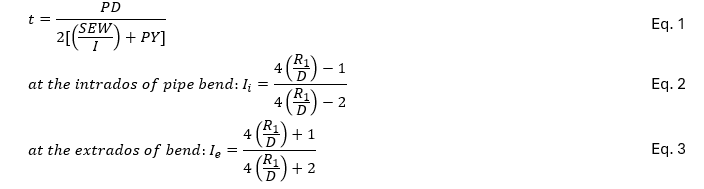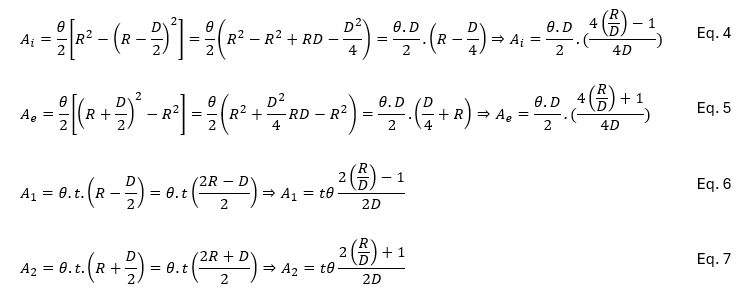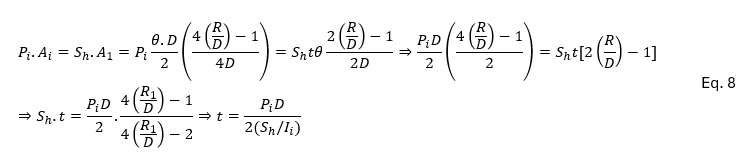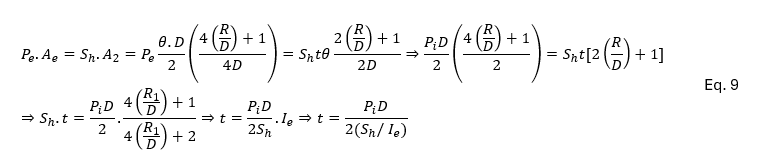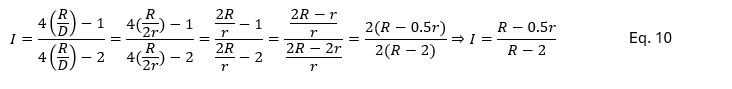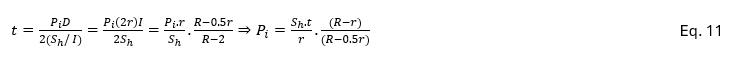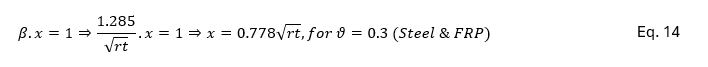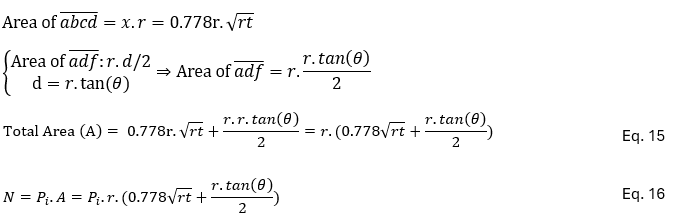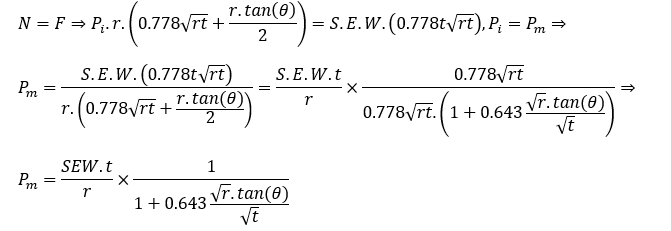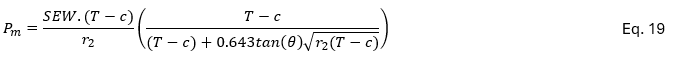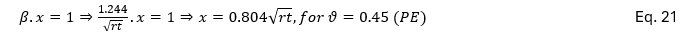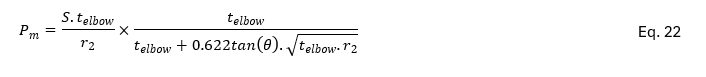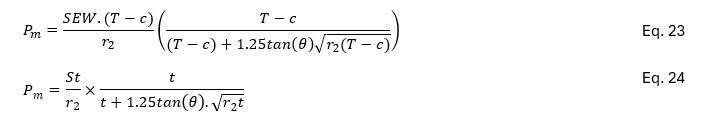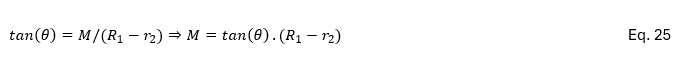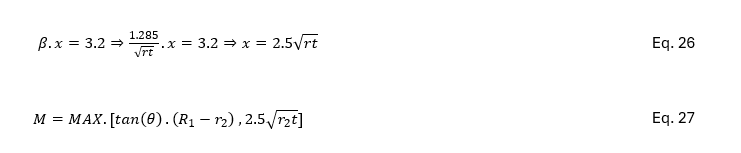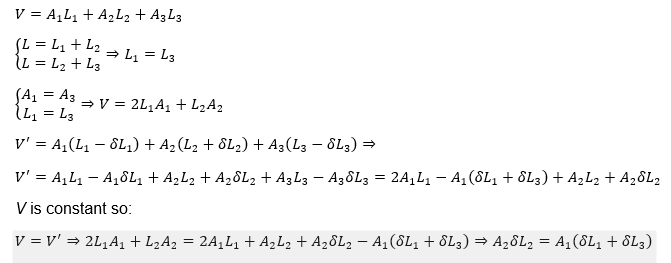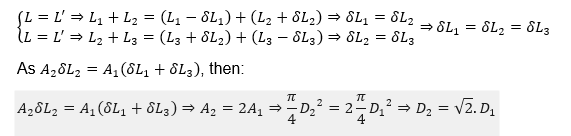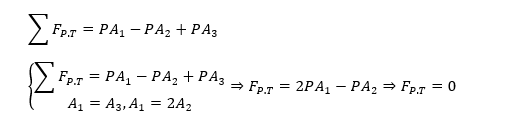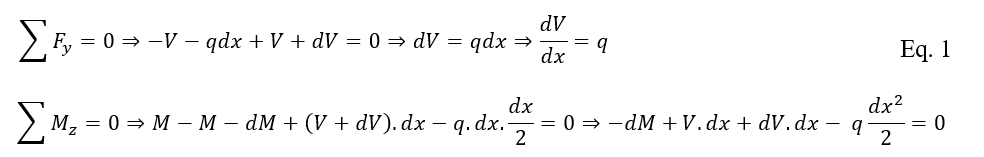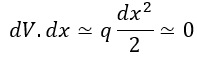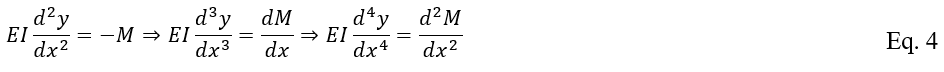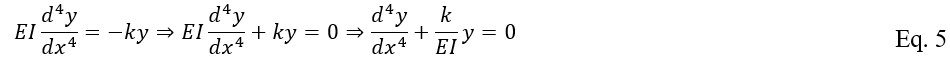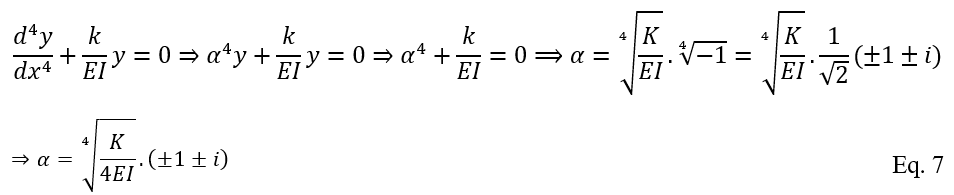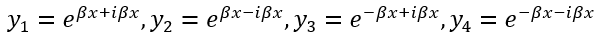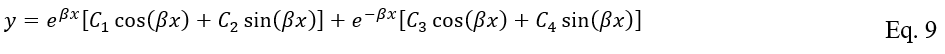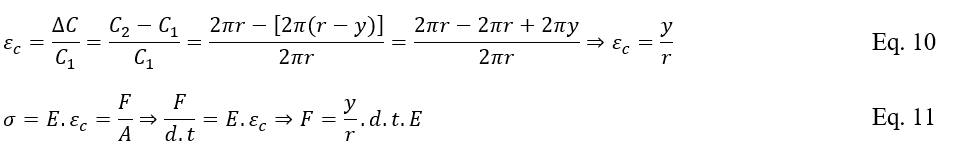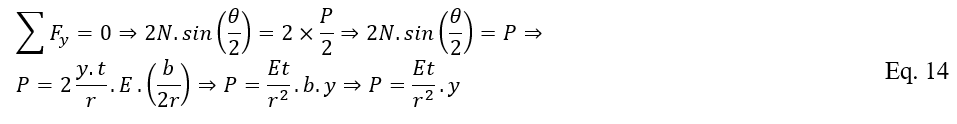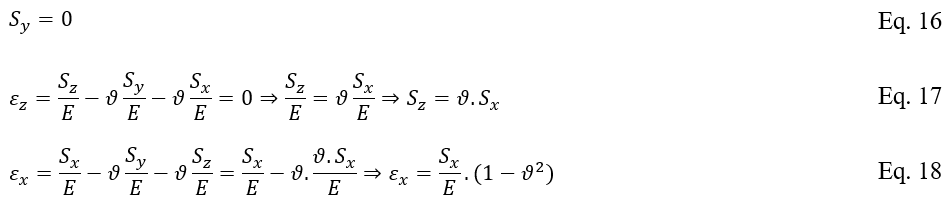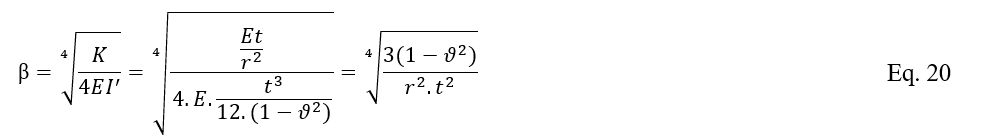Whatispiping Team, in association with Everyeng, is conducting an online pre-recorded Comprehensive Piping Stress Analysis Certificate course to help mechanical and piping engineers. Along with the regular content that the participants will be learning, there will be a dedicated 1-hour doubt-clearing session (/question-answer session) with the mentor.
Contents of Online Piping Stress Analysis with Caesar II Course
The program will be delivered using the most widely used pipe stress analysis software program, Caesar II. The full course is divided into 4 parts.
Part A will describe the basic requirements of pipe stress analysis and will help the participants to be prepared for the application of the software package.
Part B will describe all the basic static analysis methods that every pipe stress engineer must know.
Part C will give some understanding of the dynamic analysis modules available in Caesar II; and
Part D will explain all other relevant details that will prepare a basic pipe stress engineer to become an advanced user. Additional modules will be added in this section as and when ready.
In its present form, the full course will roughly cover the following details:
Part A: Basics of Pipe Stress Analysis
What is Pipe Stress Analysis?
Stress Critical Line List Preparation with Practical Case Study
Inputs Required for Pipe Stress Analysis
Basics of ASME B31 3 for a Piping Stress Engineer
ASME B31.3 Scopes and Exclusions
Why stress is generated in a piping system
Types of Pipe Stresses
Pipe Thickness Calculation
Reinforcement Requirements
ASME B31.3 Code Equations and Allowable
Introduction to Pipe Supports
Role of Pipe Supports in Piping Design
Types of Pipe Supports
List of Pipe Supports
Pipe Support Span
How to Support a Pipe?
Pipe Support Optimization Rules
Pipe Support Standard
Support Engineering Considerations
What is a Piping Isometric?
What is an Expansion Loop?
Various Bonus Lectures like Introduction to Pipe Stress, Pressure Stresses in Piping, Radial Stresses in Piping, Material Stresses in Piping, etc.
Part-B: Static Analysis in Caesar II
Introduction to Caesar II
Getting Started in Caesar II
Stress Analysis of Pump Piping System
Creating Load Cases
Wind and Seismic Analysis
Generating Stress Analysis Reports
Editing Stress Analysis Model, Trunnion Modelling
Spring Hanger Selection and Design in Caesar II
Introduction
Types of Spring Hangers
Components of a Spring Hanger
Selection of Variable and Constant Spring hangers
Case Study of Spring Hanger Design and Selection
Certain Salient Points
Flange Leakage Analysis in Caesar II
Introduction
Types of Flange Leakage Analysis and Background Theory
Case Study-Pressure Equivalent Analysis
Case Study-NC Method
Case Study-ASME Sec VIII method
Stress Analysis of PSV Piping System
Introduction
PSV Reaction Force Calculation
Applying PSV Reaction force
Practical Case Study
Certain best practices
Heat Exchanger Pipe Stress Analysis
Introduction
Creating Temperature Profile
Modeling the Heat Exchanger
Nozzle Load Qualification
Practical Case Study
Methodology for shell and tube inlet nozzle stress analysis
Vertical Tower Piping Stress Analysis
Introduction
Creating Temperature Profile
Equipment Modeling
Modeling Cleat Supports
Skirt temperature Calculation
Nozzle Load Qualification
Practical Example
Storage Tank Piping Stress Analysis
Introduction
Reason for Criticality of storage tank piping
Tank Settlement
Tank Bulging
Practical example of tank piping stress analysis
Nozzle Loading
Additional Bonus modules on Pump Piping Stress Analysis
API610 Pump nozzle evaluation using Caesar II
Part C: Dynamic Analysis is Caesar II
Introduction-Dynamic Analysis in Caesar II
Types of Dynamic Analysis
Static vs Dynamic Analysis
Dynamic Modal Analysis
Equivalent Static Slug Flow Analysis
Dynamic Response Spectrum Analysis
Part D: Miscellaneous other details
WRC 297/537 Calculation
What are WRC 537 and WRC 297?
Inputs for WRC Calculation
WRC Calculation with Practical Example
Underground Pipe Stress Analysis
Jacketed Piping Stress Analysis
Create Unit and configuration file in CAESAR II
ASME B31J for improved Method for i, k Calculation in Caesar II
Discussion about certain Questions and Answers
GRE/FRP Pipe stress analysis
GRE Pipe Stress Analysis using Caesar II
GRE Stress Analysis-Basics
FRP Pipe Stress Analysis Case Study
GRE Flange Leakage Analysis
Meaning of Stress Envelope; Understand it
Reviewing A Piping Stress System
Introduction
What to Review
Reviewing Steps
Case Study of Reviewing Pipe Stress Analysis Report
Reviewing Best Practices
FIV Study
Flow Induced Vibrations-Introduction
What is Flow-Induced Vibration (FIV)?
Flow-Induced Vibration Analysis
Corrective-Mitigation Options
AIV Study
Introduction
What is Acoustic-Induced Vibration (AIV)?
Acoustic-Induced Vibration Analysis
Corrective-Mitigation Options
Basics of Expansion Joints
Introduction-Expansion Joints
Basics of Expansion Joints
Types of Expansion Joints
Application Engineering
Design Considerations for Expansion Joints
Single Expansion Joint Modelling in Caesar II
Basics Theory of HDPE Pipe Stress Analysis
Various Bonus modules on Interview Questions, Jacketed Piping System Stress Analysis, Stress Intensification Factor, etc.
How to Enroll for this Course
To join this course, simply click here and click on Buy Now. It will ask you to create your profile, complete the profile, and make the payment. As soon as the payment is complete, you will get full access to the course. If you face any difficulty, contact the Everyeng team using the Contact Us button on their website.
Detailed Online Course on Pipe Stress Analysis (25 hours of Content) with Certificate + Free Trial Version of Pipe Stress Analysis Software
This course is created by an experienced pipe stress analysis software developer (15+ years experience), Ph.D. and covers all features of onshore above ground and underground piping and pipeline analysis. This course is based on the PASS/START-PROF software application, though it will be interesting for users of any other pipe stress analysis software tools as it contains a lot of theoretical information.
The course consists of video lectures, quizzes, examples, and handout materials.
Type: an on-demand online course.
Duration: 25 hours.
Course price:200 USD30 USD.
Instructor: Alex Matveev, head of PASS/START-PROF Pipe Stress Analysis Software development team. Always available for your questions at Udemy, LinkedIn, Facebook
Alex Matveev
Who should attend
All process, piping, and mechanical engineers specialized in design and piping stress analysis for the specified industries:
Oil & Gas (Offshore/Onshore)
Chemical & Petrochemical
Power (Nuclear/ Non-Nuclear)
District Heating/Cooling
Water treatment
Metal industry
Training software
All trainees are provided with a free 30-day pipe stress analysis software license (PASS/START-PROF). How to get a free license
Certificate
After finishing the course, you will receive Certificates from both the Udemy and from PASS Team.
How to use PASS/START-PROF software for pipe stress analysis
How to work with different load cases
How to model different types of piping supports, the spring selection
What are stress intensification and flexibility factors and how to calculate them using FEA and code requirements
How to model trunnion and lateral tees
How to model pressure vessels and columns connection: modeling local and global flexibility, WRC 297, WRC 537, FEA
How to model storage tank connection (API 650)
How to model connection to air-cooled heat exchanger API 661, fired heater API 560, API 530
How to model connection to Pump, Compressor, Turbine (API 610, API 617, NEMA SM23)
How to model buried pipelines: Submerged Pipelines, Long Radius Bends Modeling of Laying, Lifting, Subsidence, Frost Heaving, Fault Crossing, Landslide
Underground pipelines Seismic Wave Propagation, Pipe Buckling, Upheaval Buckling, Modeling of Pipe in Chamber, in Casing with Spacers. Electrical Insulation kit
Minimum design metal temperature calculation MDMT calculation, impact test
Modeling of Expansion Joints, Flexible Hoses, Couplings
Import and export to various software: CAESAR II, AVEVA, REVIT, PCF format, etc.
How to do Normal Modes Analysis and how to interpret results
ASME B31G Remaining Strength of Corroded Pipeline Calculation
A pipe bend in the oil and gas industry is a curved section of piping used to change the direction of fluid flow, typically by 45° or 90°. Pipe bends are designed to withstand high pressure, temperature, and mechanical stresses while maintaining smooth and efficient flow. They are commonly used in pipelines, process plants, refineries, and other piping systems to route fluids around equipment and structures.
The following article will explain the maximum allowable internal pressure capabilities for pipe bends used in the oil and gas industries.
Two types of bends are quite common in the oil and gas industries. Normal pipe bends as a pipe fitting and mitre bends.
1. Pipe Bends and Elbows
Minimum Required Wall Thickness (tm) of Pipe Bends
While the concept of calculating the tm (t+c) of pipe bends is similar to the calculation of pipe wall thickness, the designer shall consider the “I” factor for the intrados and extrados of the bend as follows, as per ASME B31.3:
First, it is shown what the factor “I” is. Then, the effect of this factor on the maximum allowable internal pressure (Pm) of pipe bends is evaluated.
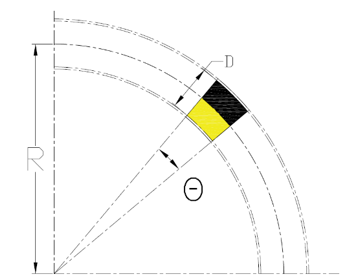
Figure 1 illustrates a simple bend under Internal Pressure (Pi). As shown, a radial pipe segment is divided into two zones: the inside zone is shown in yellow, and the outside zone is shown in black.
Figure 1. Pressure Stress at Bend
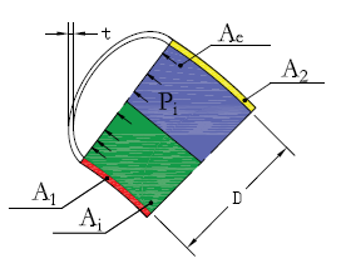
The Pi acts on the area named Ai and Ae, while the hops stress (Sh) acts on the A1 and A2, as shown in Figure 2.
Figure2. Pressured Stress at a radial Pipe Segment
Thus:
At the intrados of pipe bend:
At the extrados of pipe bend:
By comparing Equations 8 and 9 together, it is clear that the required THK. of a pipe bend at the intrados is greater than the required value at the extrados of the bend. Thus, ASME B31.3, ASME NM.1, and ASME NM.2 consider the Pm at the intrados of pipe bends. If Eq. 2 is simplified, we have:
Where R is the bend radius of the welding elbow or pipe bend, and r is the radius of pipe. It should be noted that ASME NM.2 replaces I with m in Equations 2-3-7 and 2-3-8.
To evaluate Pm, with respect to Equations 9 and 10, we have:
Based on Eq. 11, for FRP pipes (ASME NM.2, Eq. 2-3-10) and HDPE pipes (ASME NM.1, Eq. 2-3-7):
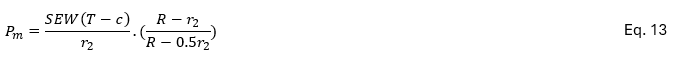
For steel pipe bends, as per ASME B31.3 [Eq. (4b)], the designer shall consider the effects of the factors E and W, and replace the t by (T-c). Thus:
Where:
E is the quality factor.
W is the weld joint strength reduction factor.
c is the sum of the mechanical allowances.
T is the wall thickness of pipe bend.
2- Miter Bends
Sometimes mitered pipe ends are connected together to make a change in the direction of piping. These mitered connections are known as mitered bends. Here, it is shown when a miter bend requires design consideration and what the requirements are.
Some standards, codes, and studies state that if the angular offset is 3 degrees or less, there is no need for any design consideration as mitered bend. For instance:
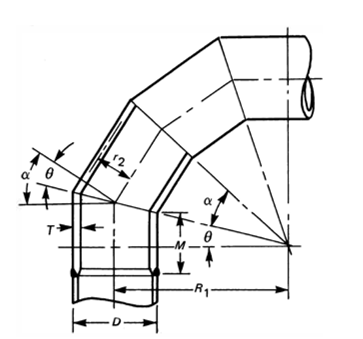
ASME B31.3-2022, Clause 304.2.3: An angular offset of 3 degrees or less (angle α in Figure 3) does not require design consideration as a miter bend.
ASME NM.1-2018, Clause 2-3.2.4, Section (e): Mitered joints of 3 degrees or less shall not require redesign consideration as mitered elbows.
Dynaflow Research Group, “Finite Element Analysis of Filament Wound Pipe Coupler”
*It should be noted that other standards or codes may specify other requirements.
Figure3Nomenclature for Miter Bends
As the pipe direction changes, the geometry changes. Therefore, in this case, the effects of the discontinuity area and, subsequently, the discontinuity stresses on the pipe and mitered elbow shall be evaluated.
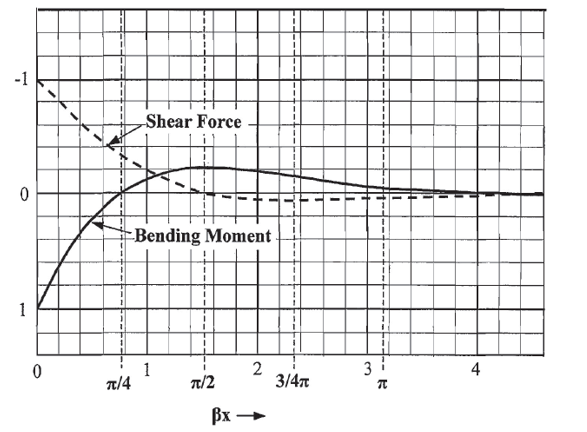
As shown in the relevant discontinuity stress post, the effective zone is a key parameter in discontinuity areas. It is good practice to consider βX=1, where the magnitude of shear stress decreases to less than 20% of its maximum value. Thus:
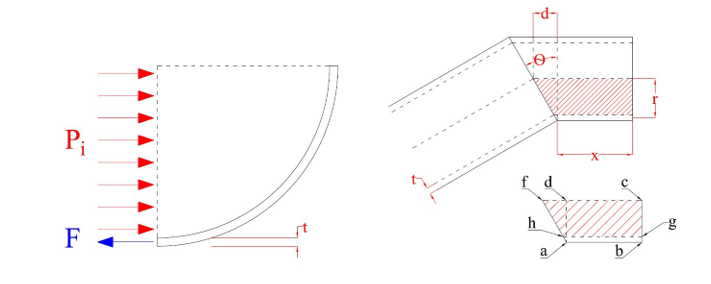
According to Figure 4, the hatched area is the smallest existing area in a mitered elbow, and therefore, it is more vulnerable than other areas to internal pressure. Therefore, the design criteria shall ensure that this area can resist Pi.
Figure 4
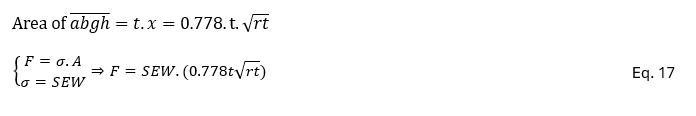
The Reaction Force (F) acts on the Area of “abgh” as shown in Figure 4, and its area is as follows:
Where:
t is the wall thickness of the pipe
Multiple Miter Bend or Single Miter Bend with Q not larger than 22.5°:
To avoid failure of the miter elbow, Pm shall be calculated as follows:
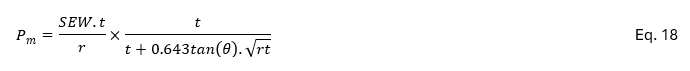
If the numerator and denominator of the fraction are multiplied by t, then:
Now, if the “t” and “r” are replaced with “T-c” and “r2”, respectively, then we have:
This is the mentioned Equation (4a) of ASME B31.3, Where:
T is the miter pipe wall thickness
r2 is the mean radius of the pipe
c is the sum of mechanical allowances
FRP pipes (Eq. 18) have no W and E factors, and if r is replaced with r2 in that equation, the Pm for FRP miter bends will be as follows:
The above equation is Eq. (2-3-9) of ASME NM.2.
It should be mentioned that for polyethylene (PE) pipes, the long-term Poisson ratio is 0.45. If this value is used, the equation 14 will be:
By considering the new value of x in the above equations, Equation 20 will be as follows:
The above equation is the referenced Equation (2-3-6) of ASME NM.1.
Equations 19, 20 and 22 are the criteria of the maximum allowable internal pressure of miter bends for steel, FRP, and HDPE pipes, respectively. While these criteria determine the Pm for miter bends, the value of Pm shall not be greater than the maximum allowable internal pressure of pipe bends (equations 12 and 13).
Single Miter Bend with θ larger than 22.5°:
ASME NM.2 and ASME B31.3 choose a more conservative approach for single miter bends with θ greater than 22.5 degrees. They almost double the 0.643 value and increase it to 1.25. Therefore, Pm for a single miter bend as per ASME B31.3 (Eq. 4c) and ASME NM.2 (Eq. 2-3-11) is, respectively, as follows:
It should be noted that ASME NM.1 limits the angle θ to 22.5 degrees.
Effective Length of the Miter-Bend Discontinuity (M)
It should be mentioned that the required thickness of steel and FRP miter bends shall be continued for an adequate distance, where the effects of discontinuity could be neglected. This distance is called “M” in ASME B31.3 and ASME NM.2. According to Figure 3, M is as follows:
Carbon equivalent (CE) is one of the most useful concepts in steel metallurgy and welding engineering. Although the name suggests that it is simply another way of expressing carbon content, its real purpose is much broader: carbon equivalent provides a convenient numerical way to estimate how carbon and other alloying elements collectively influence the hardenability, weldability, heat-affected zone (HAZ) behavior, and susceptibility to hydrogen-induced cold cracking of steel.
This becomes especially important when welding structural steels, pipelines, pressure-containing components, offshore structures, and other critical steel fabrications. A steel may have a relatively low carbon content but still exhibit challenging welding characteristics because of its manganese, chromium, molybdenum, nickel, copper, vanadium, or silicon content.
That is where the carbon equivalent formula becomes valuable.
By converting the influence of several alloying elements into a single carbon-equivalent value, engineers can compare different steel compositions and make better decisions about preheating, welding procedures, heat input, filler metals, hydrogen control, and post-weld treatment.
What Is Carbon Equivalent in Steel?
Carbon equivalent is a calculated value that represents the combined effect of carbon and selected alloying elements on a steel’s behavior.
The underlying idea is straightforward. Carbon has a major influence on the hardenability and weldability of steel, but it is not the only element that matters. Other alloying elements can also increase hardenability. Therefore, rather than considering each element independently, a carbon equivalent formula assigns different weighting factors to the elements and expresses their combined effect as an equivalent carbon percentage.
In practical terms:
Carbon equivalent tells us how the alloying chemistry of a steel behaves, from a hardenability and weldability perspective, compared with a simpler carbon steel.
The concept was originally developed to provide a numerical indication of the carbon content that would produce a similar level of hardenability. It was subsequently extended to help assess the susceptibility of steel to hydrogen cracking during welding. Carbon-equivalent relationships can also be associated with properties such as hardness, toughness, and strength.
This is why carbon equivalent is particularly important in steel welding.
Why Is Carbon Equivalent Important for Weldability?
When steel is welded, the area immediately surrounding the weld experiences rapid heating followed by cooling. This produces changes in the microstructure of the heat-affected zone (HAZ).
If the steel has sufficient hardenability, rapid cooling can result in the formation of hard microstructures such as martensite. A hard HAZ is generally less forgiving when hydrogen and residual stresses are present, increasing the possibility of hydrogen-induced cold cracking.
Consequently, a higher carbon equivalent generally indicates:
Greater hardenability
Greater potential HAZ hardness
Increased welding difficulty
Greater susceptibility to hydrogen-assisted cold cracking
A greater possibility that preheating or other welding controls will be required
Carbon equivalent is therefore an important screening parameter when assessing whether a particular steel can be welded using a proposed procedure.
However, it is important to remember that CE is not a complete weldability assessment by itself. Actual cracking susceptibility also depends on factors such as hydrogen level, restraint, cooling rate, heat input, plate thickness, joint configuration, and welding procedure.
Carbon Equivalent Formula: The Most Common Equations
There is not one universal carbon equivalent formula for every steel and every application.
Different formulas were developed for different purposes, steel compositions, and ranges of carbon content. Two of the most widely encountered equations are the IIW carbon equivalent and the AWS-type carbon equivalent.
1. IIW Carbon Equivalent Formula
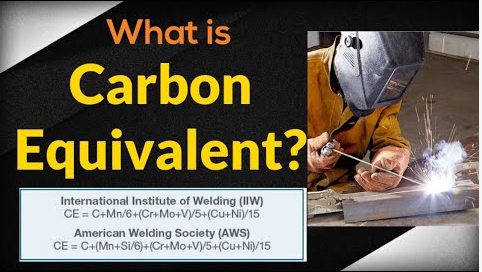
The International Institute of Welding (IIW) carbon equivalent is commonly expressed as:
CEIIW = C + Mn/6 + (Cr + Mo + V)/5 + (Cu + Ni)/15
Where:
C = carbon content, %
Mn = manganese content, %
Cr = chromium content, %
Mo = molybdenum content, %
V = vanadium content, %
Cu = copper content, %
Ni = nickel content, %
This equation became a widely accepted measure of steel weldability after the IIW adopted a simplified form of the earlier Dearden and O’Neill relationship. It has subsequently appeared in various standards and welding codes.
Example of IIW Carbon Equivalent Calculation
Suppose a steel has the following chemical composition:
This type of calculation demonstrates how a steel containing relatively little carbon can still have a meaningful carbon equivalent because of its alloying elements.
2. AWS Carbon Equivalent Formula
Another commonly referenced equation is the AWS form:
CEAWS = C + (Mn + Si)/6 + (Cr + Mo + V)/5 + (Cu + Ni)/15
The key difference is that silicon is included with manganese in the first alloying-element term.
The AWS equation therefore gives a somewhat different result from the IIW equation for the same chemical composition, particularly when silicon content is significant.
This difference illustrates an important point:
Never compare carbon-equivalent values without checking which formula was used.
A reported value such as CE = 0.40 is incomplete engineering information unless the calculation method or applicable standard is also known.
Carbon Equivalent vs Carbon Content: What Is the Difference?
It is easy to confuse carbon content with carbon equivalent, but they are not the same thing.
Carbon content is the actual percentage of carbon present in the steel.
Carbon equivalent is a calculated value that considers carbon plus the effects of selected alloying elements.
For example, two steels could contain approximately the same amount of carbon but have different levels of manganese, chromium, molybdenum, nickel, copper, or vanadium.
Their carbon contents might look similar on a material certificate, yet their hardenability and welding behavior could be substantially different.
Carbon equivalent provides a way to capture some of those differences in a single number.
Understanding Carbon Equivalent and Weldability Ratings
A commonly published classification associates carbon-equivalent ranges with general weldability:
Carbon Equivalent
General Weldability
Up to 0.35
Excellent
0.36–0.40
Very good
0.41–0.45
Good
0.46–0.50
Fair
Above 0.50
Poor
These ranges are useful as a general guide, but they should not be treated as universal acceptance limits for every steel, thickness, welding process, or code.
For example, a steel with a CE of 0.48 should not automatically be rejected for welding. Instead, the value should trigger a more careful review of the welding procedure and conditions.
Depending on the material and application, controls may include:
Preheating
Controlled interpass temperature
Appropriate heat input
Low-hydrogen consumables
Proper consumable storage
Hydrogen control
Controlled cooling
Post-weld heat treatment where required
Suitable joint design
Welding procedure qualification
The objective is not simply to achieve a low CE number; it is to control the complete set of factors that determine cracking risk.
Why High Carbon Equivalent Can Increase Hydrogen Cracking Risk
One of the most important reasons engineers calculate CE is to evaluate the potential for hydrogen-assisted cold cracking.
Three conditions are particularly important in this type of cracking:
A susceptible microstructure, often associated with high HAZ hardness
The presence of diffusible hydrogen
Tensile stresses or restraint
Carbon equivalent helps address the first part by providing an indication of hardenability and the potential for HAZ hardness.
During welding, hydrogen can enter the weld region from several sources, including moisture and contamination. If the HAZ cools rapidly and forms a hard microstructure while hydrogen remains available and tensile stresses are present, cracking may develop.
This explains why carbon equivalent and hydrogen control are closely connected in welding engineering.
Why There Are Several Carbon Equivalent Formulas
A common question among engineers and welding professionals is:
Why not simply use one carbon equivalent equation for all steels?
The reason is that steel compositions have evolved considerably, and different formulas were developed using different datasets and for different purposes.
The classic IIW equation works well for many conventional carbon and low-alloy steels. However, its applicability becomes less ideal for some modern low-carbon high-strength steels.
For example, the Pcm formula developed by Ito and Bessyo was designed using a wider range of steels and is particularly associated with modern low-carbon steels, including steels commonly used in pipeline manufacturing. TWI notes that Pcm is generally used for modern steels with carbon contents of approximately 0.11 wt% or lower.
Other formulas include:
Pcm
CEq
CEN
CEw
CET
CEIIW
Other composition- or application-specific carbon equivalents
The existence of these equations is not a sign that carbon equivalent is unreliable. Instead, it reflects the fact that different steel chemistries behave differently during welding.
Pcm Formula and Modern Low-Carbon Steels
The Pcm, or critical metal parameter, is particularly relevant when dealing with modern low-carbon steels.
Unlike the traditional IIW equation, Pcm gives greater relative importance to carbon and uses different coefficients for the alloying elements.
A commonly used form is:
Pcm = C + Si/30 + (Mn + Cu + Cr)/20 + Ni/60 + Mo/15 + V/10 + 5B
Here, boron is also included, which is significant because even small additions of boron can influence hardenability.
The Pcm approach was developed specifically to improve assessment for steels where the conventional IIW carbon equivalent is less suitable.
This is particularly important in modern pipeline and high-strength steel applications, where carbon levels may be deliberately kept low while strength is achieved through controlled alloying and processing.
What Is CEN Carbon Equivalent?
Another carbon-equivalent approach is CEN, developed to evaluate the weldability of a wide variety of steels.
An interesting feature of CEN is that its relationship with other carbon equivalents changes depending on carbon content.
For steels with carbon content at or below approximately 0.17%, research discussed by TWI indicates a relationship between CEN and Pcm:
CEN = 2Pcm − 0.092
For carbon contents at or above approximately 0.17%, the relationship becomes closer to the IIW carbon equivalent:
CEN = CEIIW + 0.012
These relationships demonstrate why selecting an appropriate carbon-equivalent equation is important rather than treating every CE calculation as interchangeable.
Carbon Equivalent and Heat-Affected Zone Hardness
The HAZ is one of the most important regions to consider when welding steel.
Unlike the weld metal, the HAZ is not intentionally deposited. Instead, it is the parent material whose microstructure is changed by the heat of welding.
If the steel has high hardenability and the cooling rate is sufficiently fast, hard transformation products can form.
Carbon equivalent is useful because alloying elements that increase hardenability contribute to the calculated CE.
This is a simplified relationship rather than a guarantee of cracking. Cooling rate, thickness, heat input, preheat, restraint, hydrogen concentration, and the actual steel microstructure all influence the final result.
How Carbon Equivalent Helps Determine Preheat Requirements
One of the most practical applications of carbon equivalent is helping engineers determine whether preheating should be considered.
Preheating slows the cooling rate after welding. A slower cooling rate can reduce the likelihood of forming excessively hard HAZ microstructures and can also provide more opportunity for hydrogen to diffuse away before it contributes to cracking.
As a general concept, increasing CE often means that greater attention must be paid to preheat and welding procedure control.
Some commonly cited guidance indicates that preheat may become relevant as CE moves into approximately the 0.40–0.60 range, with more stringent measures potentially required at still higher values. However, actual preheat requirements must come from the applicable welding code, material specification, thickness, restraint, process, and qualified welding procedure rather than from CE alone.
Carbon Equivalent in Pipeline and Structural Steel
Carbon equivalent is particularly significant in industries where large quantities of steel must be welded reliably.
These include:
Oil and Gas Pipelines
Pipeline steels often use modern low-carbon compositions to balance strength, toughness, and weldability. Pcm and other modern carbon-equivalent approaches can therefore be particularly useful.
Structural Steel
Bridges, buildings, towers, platforms, and industrial structures may contain substantial quantities of welded steel. CE provides a useful indicator when reviewing material chemistry and welding requirements.
Pressure Vessels
Pressure-containing equipment demands careful control of welding metallurgy. Carbon equivalent can form part of the material and welding assessment.
Offshore Structures
Offshore components face demanding structural-integrity requirements. Weldability, hydrogen control, toughness, and cracking resistance are particularly important.
Heavy Equipment and Machinery
Large fabricated machinery frequently involves thick steel sections, where cooling rates and hardenability can become important considerations.
Carbon-equivalent calculations therefore have applications across a broad range of fabrication and manufacturing industries.
Using the general classification above, this falls within the very good weldability range.
But this does not mean that the steel can automatically be welded without preheat or other precautions. The actual welding procedure still needs to consider material thickness, joint restraint, hydrogen level, heat input, ambient conditions, consumables, and the governing standard.
How to Interpret a Carbon Equivalent Value Correctly
A CE value should be treated as a decision-support parameter, not a standalone pass/fail number.
When reviewing a material certificate, consider the following sequence:
Step 1: Verify the Chemical Composition
Obtain the actual or certified percentages of the relevant alloying elements.
Step 2: Identify the Correct Formula
Determine whether the applicable specification calls for IIW CE, AWS CE, Pcm, CEN, or another parameter.
Step 3: Calculate the Value
Use consistent units and chemical-analysis values.
Step 4: Compare Against Applicable Guidance
Do not automatically apply a generic CE threshold if the project specification or welding code provides different requirements.
Where necessary, introduce preheat, low-hydrogen practices, controlled interpass temperature, appropriate consumables, or other procedure requirements.
This approach is much safer than treating CE as the only determinant of weldability.
Carbon Equivalent Is Not Just a Number
The biggest misconception about carbon equivalent is that it provides a complete description of how a steel will behave during welding.
It does not.
A CE calculation is based primarily on chemical composition. But welding behavior is also governed by thermal history and mechanical conditions.
For example, two components with identical chemistry can experience different cracking risks if:
One is much thicker than the other
One joint has substantially greater restraint
One welding procedure introduces more hydrogen
One weld cools much faster
Different welding consumables are used
Preheat temperatures differ
Heat input differs significantly
Therefore, carbon equivalent should be viewed as one component of a broader weldability assessment.
Modern Steelmaking Makes Carbon Equivalent Even More Relevant
Modern steelmaking increasingly uses carefully controlled alloying and processing to achieve high strength without simply increasing carbon content.
This creates steels with relatively low carbon but carefully selected additions of manganese, chromium, nickel, molybdenum, vanadium, and other elements.
Consequently, simply looking at the carbon percentage can give an incomplete picture of welding behavior.
Carbon-equivalent calculations provide a convenient way to interpret the combined contribution of these elements.
Modern analytical technologies can also determine elemental composition rapidly and calculate carbon equivalence automatically when an appropriate formula has been specified.
Key Takeaways About Carbon Equivalent in Steel
Carbon equivalent is an essential concept for anyone involved in steel welding, metallurgy, fabrication, pipelines, structural engineering, or materials selection.
The most important points are:
Carbon equivalent combines the effects of carbon and selected alloying elements into a single value.
Higher CE generally indicates greater hardenability and potentially greater welding difficulty.
CE is strongly associated with HAZ hardness and hydrogen-induced cold-cracking susceptibility.
The IIW formula is one of the most widely used carbon-equivalent equations.
The AWS equation differs from the IIW equation by including silicon with manganese.
Pcm is particularly relevant to modern low-carbon steels.
CEN, CEq, CEw, CET, and other formulas have been developed for specific steel types or assessment purposes.
A CE value should never be interpreted without knowing which formula produced it.
Preheat, hydrogen control, heat input, thickness, restraint, and cooling rate must also be considered.
Carbon equivalent is a useful engineering indicator, but it is not a complete weldability assessment.
Final Thoughts
When steel is welded, chemistry matters—but chemistry is only the beginning of the story.
The carbon equivalent concept provides engineers with a practical bridge between chemical composition and welding behavior. By converting the combined influence of alloying elements into a single calculated parameter, it becomes much easier to compare steels, anticipate hardenability, identify potential HAZ problems, and establish appropriate welding controls.
The most important lesson is not simply to memorize one carbon equivalent formula. It is to understand why different formulas exist and when each one is appropriate.
For conventional steels, the IIW or AWS-style equations may provide a useful starting point. For modern low-carbon steels, particularly those used in demanding pipeline applications, parameters such as Pcm and CEN may offer a more appropriate assessment. Technical guidance from welding organizations emphasizes that the suitability of a particular carbon equivalent depends on the steel composition and the purpose for which the calculation is being used.
Ultimately, a good welding decision combines carbon equivalent, material thickness, welding procedure, hydrogen control, cooling conditions, restraint, and applicable codes and standards.
That is why carbon equivalent remains such an important tool in modern welding engineering: it turns a complex chemical composition into a practical engineering indicator—helping fabrication professionals make more informed decisions before the welding arc is ever struck.
Modeling of In-line Pressure-Balanced Expansion Joint in Caesar II
A pressure-balanced expansion joint is a type of piping expansion joint designed to absorb thermal expansion while preventing the expansion joint from creating a large pressure-induced force on the piping or equipment.
Why a Pressure-Balanced Expansion Joint is needed
When a pipe contains a pressurized fluid, pressure acting on an ordinary bellows creates an end force: F=P×A
where:
F = pressure thrust
P = internal pressure
A = effective area of the bellows
For high-pressure piping, this force can be very large and would normally have to be resisted by anchors and structural supports.
A pressure-balanced expansion joint uses additional bellows and a balancing arrangement so that the pressure thrust from one bellows is largely cancelled by an opposing pressure thrust.
Types of Pressure-Balanced Expansion Joint
Two types of pressure-balanced expansion joints are widely used in oil and gas industries. They are classified mainly by how the balancing bellows are arranged and what pipe movement they accommodate.
1. Elbow Pressure-Balanced Expansion Joint
This is one of the most common arrangements.
It typically consists of:
A main flow bellows
A balancing bellows
An elbow
Tie rods/linkages connecting the two bellows
The balancing bellows generates an opposing pressure thrust, so the net pressure force transmitted to the piping is greatly reduced.
Used for: axial thermal movement, especially where an anchor cannot conveniently absorb the pressure thrust.
2. In-Line Pressure-Balanced Expansion Joint
The main and balancing bellows are arranged in line with the pipe.
The pressure thrust from the working bellows is balanced by the pressure thrust from the balancing bellows.
Used for: mainly axial movement in relatively straight piping systems.
A simplified arrangement is:
Pipe → Main Bellows → Balance Bellows → Pipe
Some More Details about In-line Pressure Balanced Expansion Joints
When the expansion joint is installed in a straight pipeline, it is called an In-Line Pressure Balanced Expansion Joint (IPBEJ).
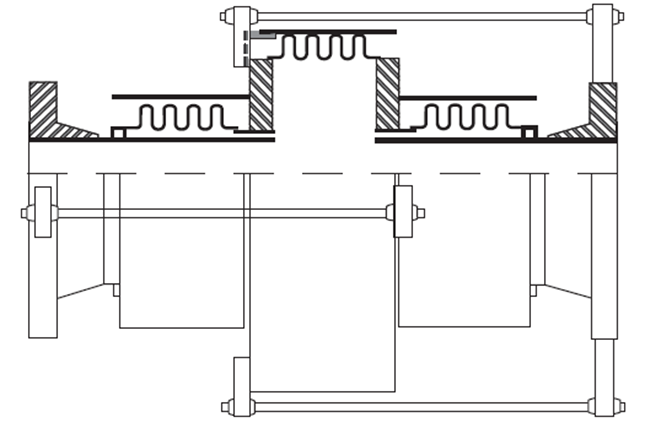
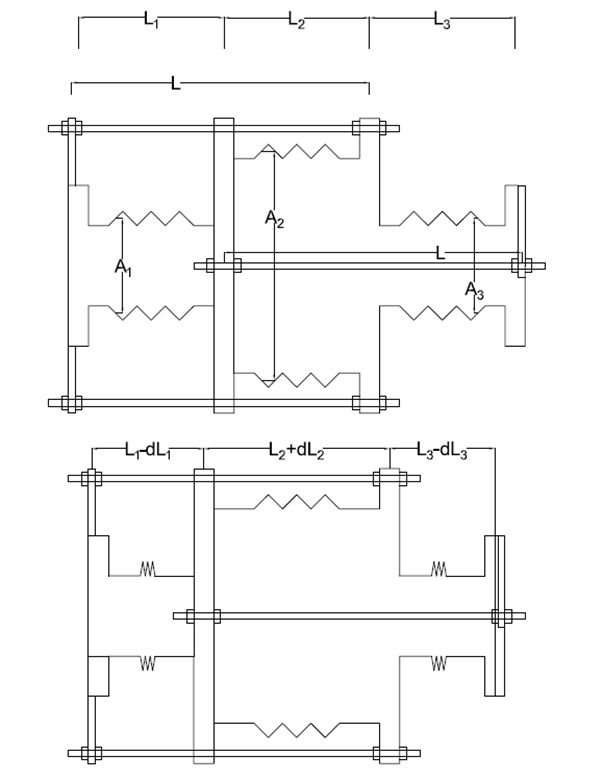
The IPBEJ consists of two smaller bellows placed on either side and one bigger bellows placed in the middle. They are connected by the use of Tie-Rods as shown in Figure 1. So, when the smaller bellows are compressed, the bigger one extends and vice versa.
Figure 1. IPBEJ Arrangement
Since the internal volume is constant, the effective area of the larger bellow is twice the effective area of each smaller bellows (Figure 2):
Figure 2. Compressed IPBEJ
In addition, the length of Tie-Rods is constant, so:
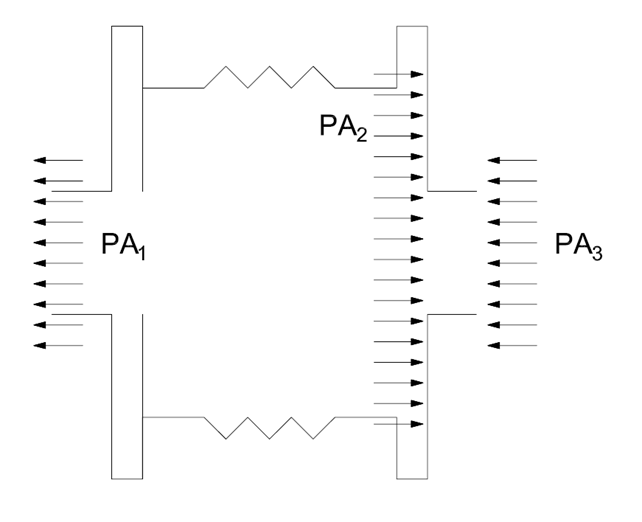
It is concluded that the Pressure Thrust Force (FPT) that either pipe ends receive is zero (Figure 3):
Figure 3. Balancing the pressure thrust
Modelling an In-Line Pressure Balanced Expansion Joint in CAESAR II
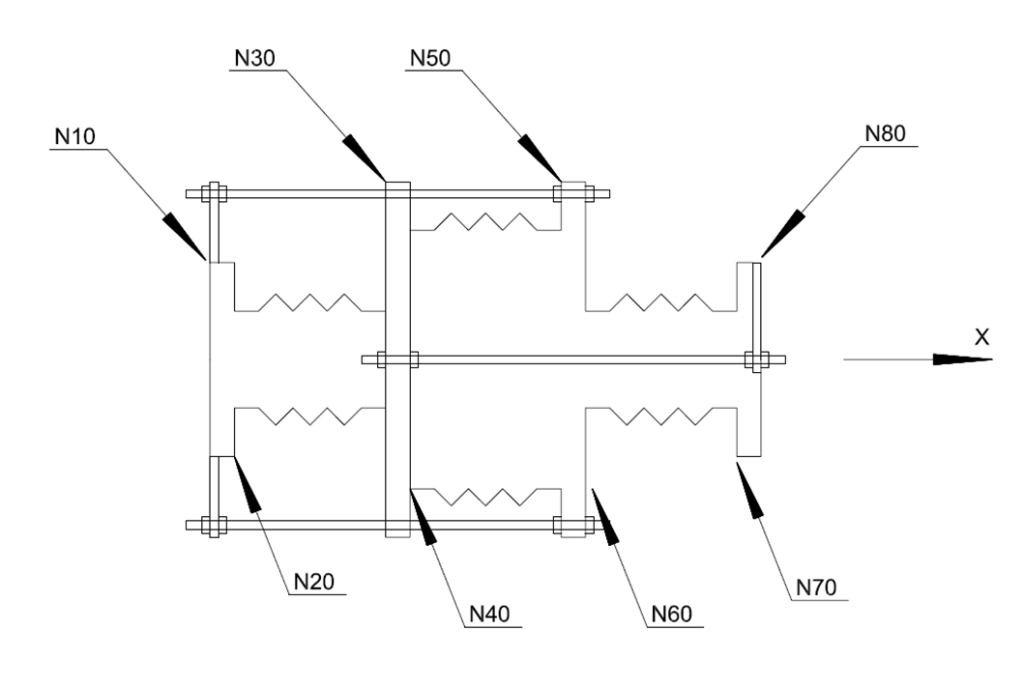
Let’s assume that the IPBEJ has 4 Tie-Rods and we want to model the IPBEJ from node number 10 to node number 80 along the +X direction as shown in Figure 4.
Follow the steps below:
Figure 4. IPBEJ main node numbers
Element 10 to 20: Rigid element for first flange with total weight divided by 4. Length according to the data sheet along the +X direction.
Element 20 to 30: Expansion Joint with determined spring rates and effective diameter A1. Length according to the data sheet along the +X direction.
Element 30 to 40: Rigid element for second flange with total weight divided by 4. Length according to the data sheet along the +X direction.
Element 40 to 50: Expansion Joint with determined spring rates and effective diameter A2. Length according to the data sheet along the +X direction.
Element 50 to 60: Rigid element for third flange with total weight divided by 4. Length according to the data sheet along the +X direction.
Element 60 to 70: Expansion Joint with determined spring rates and effective diameter A1. Length according to the data sheet along the +X direction.
Element 70 to 80: Rigid element for fourth flange with total weight divided by 4. Length according to the data sheet along the +X direction.
Now the Tie-Rods can be modelled as follows:
Element 10 to 90: Zero-weight rigid element. Length according to the data sheet along the +Y direction.
Element 60 to 100: Zero-weight rigid element. Length according to the data sheet along the +Y direction.
Element 90 to 110: Zero-weight rigid element. Length from node 10 to node 60 along the +X direction.
Element 10 to 120: Zero-weight rigid element. Length according to the data sheet along the -Y direction.
Element 60 to 130: Zero-weight rigid element. Length according to the data sheet along the -Y direction.
Element 120 to 140: Zero-weight rigid element. Length from node 10 to node 60 along the +X direction.
Element 30 to 150: Zero-weight rigid element. Length according to the data sheet along the +Z direction.
Element 80 to 160: Zero-weight rigid element. Length according to the data sheet along the +Z direction.
Element 150 to 170: Zero-weight rigid element. Length from node 30 to node 80 along the +X direction.
Element 30 to 180: Zero-weight rigid element. Length according to the data sheet along the -Z direction.
Element 80 to 190: Zero-weight rigid element. Length according to the data sheet along the -Z direction.
Element 180 to 200: Zero-weight rigid element. Length from node 30 to node 80 along the +X direction.
Notes:
1- The temperature of Tie-Rods shall be at ambient temperature; the OD and THK can be modelled with the OD of the Tie-Rod, and THK can be half of the OD, and the pressure can be set as zero.
2- Weight of the fluid inside the IPBEJ depends on the specified OD and thickness of the elements. Therefore, it is more accurate to determine the OD and THK of bellows as determined in the technical offer and/or data sheet.
Now the restraints of Tie-Rods shall be determined as follows:
Node 110 to 100: ANC in the X direction, RY, and RZ.
Node 140 to 130: ANC in the X direction, RY, and RZ.
Node 170 to 160: ANC in the X direction, RY, and RZ.
Node 200 to 190: ANC in the X direction, RY, and RZ.
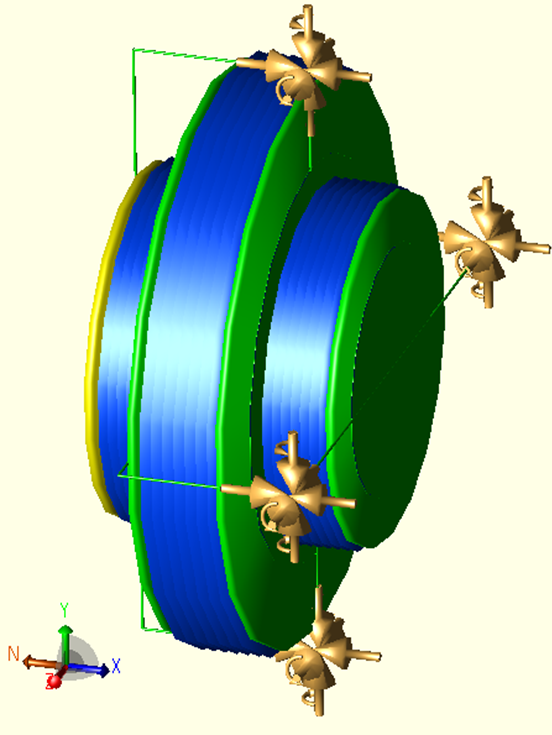
Fig. 5: Typical In-line Pressure Balanced Expansion Joint in Caesar II
References:
Pipe Stress Engineering by Peng
Standards of the Expansion Joint Manufacturers Association, EJMA -9TH Edition
https://usbellows.com
What is Discontinuity Stress with respect to Pipe Stress Analysis?
A discontinuity occurs where there is a sudden change in material, geometry, or loading. The behaviour of different free components, such as their displacement under a specific load, may be different. However, when they are connected, they cannot move freely. This restriction of movement creates stresses, which are referred to as discontinuity stresses.
Beams on Elastic Foundation Theory
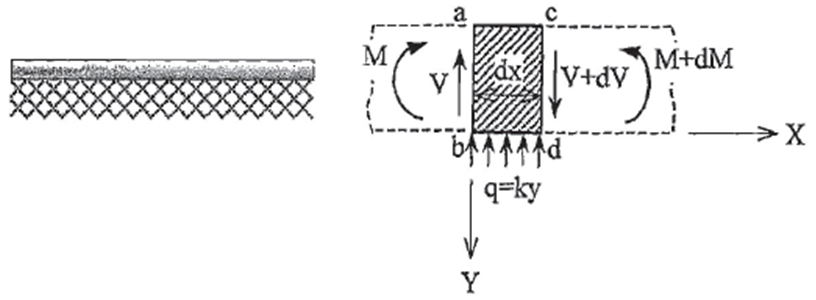
Beams on Elastic Foundation theory is used to evaluate the discontinuity stress. Figure 1 shows an infinitely small beam element placed on an elastic foundation.
Figure 1 Beam on Elastic Foundation
As it is shown, the distributed force q, acts upwards in response of the downward displacement of the element.
q=ky,
Where:
K is the spring constant per unit length
y is the vertical displacement of the element
Force and moment equilibrium of the element show in the Figure 1 is as follows:
The second order of very small quantities can be ignored, so:
Therefore:
Combining Eqs. 1 and 2:
The displacement made by shear force is insignificant in a slender beam. Thus, it can be assumed that the displacement is completely due to bending moment.
Combining Eqs. 3 and 4:
The equation 5 can be solved if y=eex, where α is an exponent constant that must be determined. Differentiating eαx four times with respect to x and substituting y, we have:
From Eqs. 5 and 6:
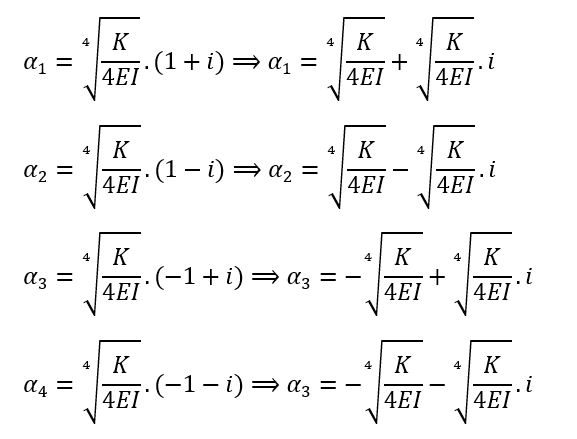
The answers of Eq. 7 are:
By considering the characteristic factor β=4√(k/4EI), and since y=eex, we obtain:
and:
Where A, B, C, and D are integration constants. By performing some mathematical manipulation, we have:
Determination of the integration constants C1, C2, C3, and C4 depends of boundary conditions of the beam. This equation is used to solve some of the discontinuity stress problems in the piping field.
Using Beam on Elastic Foundation in Cylindrical Shells
The beam on elastic foundation theory can be used for evaluation of discontinuity stresses of a thin-wall cylindrical shell.
Before conducting any calculations, it must be shown that the behaviour of shell is similar to that of a beam on an elastic foundation. Once it is established, the spring constant can be used in the further calculations. With respect to the Figure 2, we have:
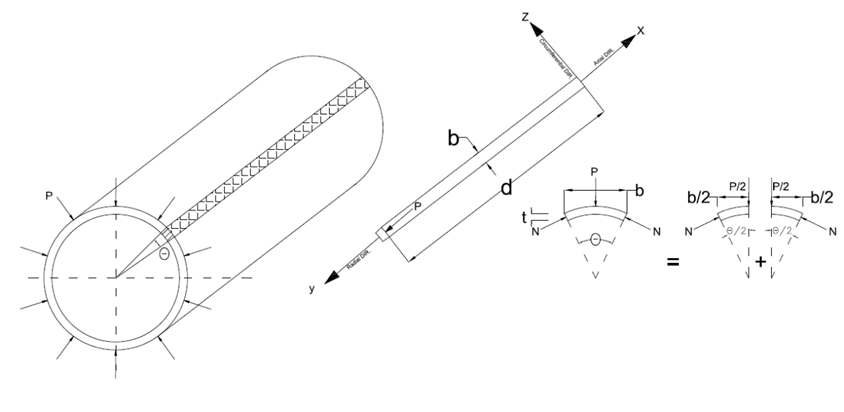
Figure 2 Cylindrical Shell with Axially Symmetrical Loading
The radial load P is uniformly distributed along circles perpendicular to the axis of the cylinder. The loading is symmetrical; so, the section will remain circular. The load P moves the shell by a distance y towards the center. The magnitude of the radial displacement decreases from y to zero as the distance from the point load increases along the axial direction. This change in displacement creates bending stress in the shell. Since the cross-section and loading are symmetrical, it can be assumed that the situation is similar to that of a longitudinal strip of unit width, b.
The load reduces the radius of the cross-section and its circumference. Further calculations evaluate the circumferential strain (εc), the circumferential compressive force (F), and the support force per unit length (P).
Based on the Eq. 11, the Circumferential Compressive Force per unit strip length (N) is:
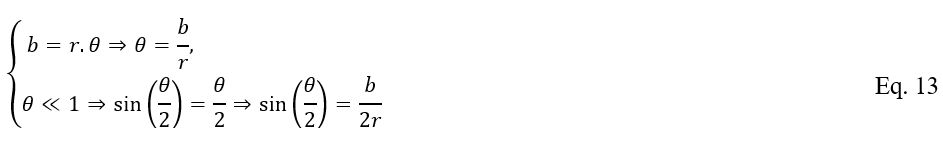
In addition, the width of the strip, b =r.(Theta). So:
Applying force equilibrium, combining Eqs. 12 and 13, and considering b = 1, we obtain:
As shown, P is proportional to y. Therefore, the strip can be considered as a beam on an elastic foundation. Thus, the spring constant for the unit width is:
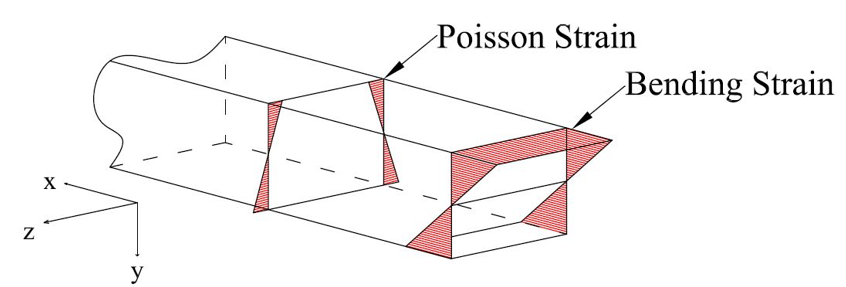
According to Figure 4, if the element is free to move along the Z direction, the bending moment will cause a strain in the Z direction (εZ).
Figure 3 Sideway Constriction
In a cylindrical shell, the cross-section remains circular. Thus, the εZ equals to zero. In addition, the radial stress (Sy) is neglected. Therefore, the strain along the axial axis of the shell (εX) is as follows:
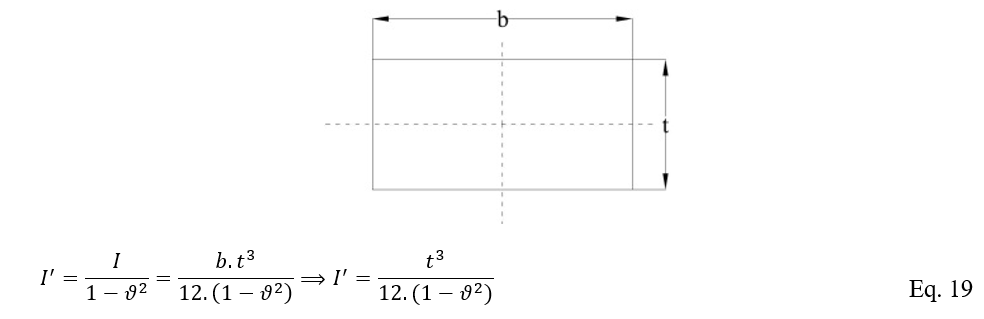
The result shows that for a laterally restricted beam, the εX is smaller than εX predicted by Hook’s low by a factor of (1-v2). In other words, a laterally restricted beam is stiffer than a free beam. To compensate for the reduction in strain, the flexural rigidity (EI) must be increased by a factor 1/(1-v2). This can be achieved by increasing either E or I. For simplicity, it is recommended to increase the moment of inertia, I. Thus, for the rectangular cross-section of a beam with unit width (b=1), the moment of inertia is as follows:
By combining the Eqs. 15 and 19, the β is as follows:
If the value of v is assumed to be 0.3, then the β=1.285/√(r.t)
Effective Width of Discontinuity Area
Once the β is evaluated, another key parameter, known as the effective width (x), must be determined, for example when reinforcement is required. The effect of discontinuity decreases exponentially as the distance from the discontinuity increases. It reduces rapidly but never completely disappears. Thus, an effective zone is considered to account for the discontinuity area.
Owing to the uncertainty regarding the effective zone, each situation requires a specific method for defining an appropriate effective zone. For example, one suitable criterion is the distance where the shear force becomes less than 20% of the maximum shear force, or the bending moment becomes less than the 21% of the maximum bending moment.
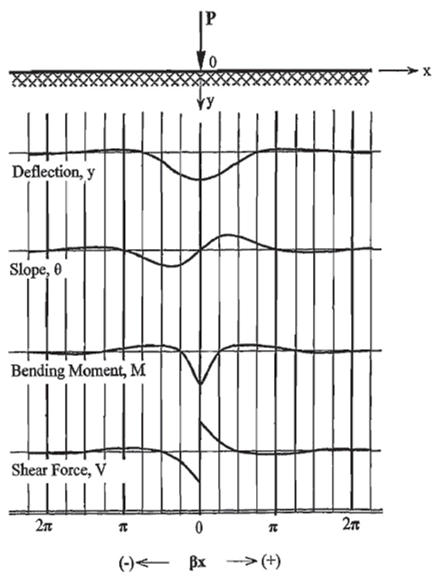
Figure 4 shows the deflection, slope, bending moment and shear force along the beam in terms of the dimensionless parameter βx (x is the distance from the discontinuity point). It should be noted that the P curves reflect only the general shapes.
Figure 4 Infinite Beam with Concentrated Force
With respect to the symmetry of the beam and the importance of the shear force and bending moment, Figure 5 provides an enlarged view of the attenuation. Based on this figure, the magnitude of the shear force becomes less than 20% of its maximum value when βx is more than 1, and the bending moment becomes less than 21% of its maximum value when βx is more than (pi)/2.
Figure 5 Attenuation of Shear Force and Bending Moment
References
Pipe Stress Engineering – L.C. Peng and T.L. Peng
What is Octave Aspect Pipe Stress? The Evolution of CAESAR II
For decades, “CAESAR II” has been one of the most widely used names in pipe stress analysis, supporting projects across industries, including refining and power generation. In 2026, as Hexagon prepared the transition of its Asset Lifecycle Intelligence portfolio under the Octave brand, CAESAR II was reintroduced as Octave Aspect Pipe Stress (formerly CAESAR II).
If you’re an engineer wondering what changed, or you’re evaluating pipe stress analysis tools for the first time, this guide walks through what “Octave Aspect Pipe Stress” is, what it does, and how it relates to CAESAR II.
The Rebranding: Why the Change?
The shift from CAESAR II to Octave Aspect Pipe Stress is more than a name update. It aligns the product with Octave’s Aspect engineering analysis portfolio and Octave’s broader software brand.
Octave positions Aspect Pipe Stress as a modern pipe stress analysis solution that supports global codes and standards and integrates with Octave design and analysis tools, including Octave Forte 3D and Octave Forte 3DWorx, to streamline workflows and reduce rework.
Core Capabilities of Octave Aspect Pipe Stress
At its core, Aspect Pipe Stress is a comprehensive pipe stress analysis solution that enables engineers to model, evaluate, and report on piping systems of any size under a wide range of operating and environmental conditions.
1) Static and dynamic analysis
Aspect Pipe Stress supports both static and dynamic analysis, including common real-world loading scenarios such as:
Weight, pressure, and thermal loads
Wind/wave and seismic loads (as applicable)
Dynamic analysis, including modal, response spectrum, harmonic, and time history methods
2) Global code and standards support
Aspect Pipe Stress supports dozens of international piping codes and standards (Octave cites 35+ and also references 50+), helping teams standardize analysis across global projects.
3) Equipment and connection checks (via auxiliary modules)
Beyond the piping model, Aspect Pipe Stress includes auxiliary capabilities for:
Equipment nozzle analysis (per multiple industry standards)
Flange analysis (including ASME and EN 1591)
Key Features of Octave Aspect Pipe Stress
Aspect Pipe Stress combines proven pipe stress analysis capabilities with workflow features designed to reduce rework and improve model quality.
Collaboration and interoperability
Aspect Pipe Stress supports cross-discipline workflows through bidirectional integrations with tools like Aspect Pressure Vessel and interoperability with design solutions such as Octave Forte 3D and Octave Forte 3DWorx, helping keep design and analysis data aligned.
Model validation
Aspect Pipe Stress includes built-in error checking and clash detection to help identify issues early and avoid interference with critical equipment.
Integration with Octave design tools
Aspect Pipe Stress can exchange piping design data with Octave design solutions (including Forte 3D and Forte 3DWorx), helping streamline handoffs between design and stress analysis and reducing duplicate data entry.
Other important features are:
Quality assurance and regulated-industry readiness: Aspect Pipe Stress is developed and maintained under a QA program that cites ASME NQA-1, plus 10 CFR Part 21 and 10 CFR Part 50 Appendix B, and the team is conformant with ISO 9001. (This is a strong differentiator for nuclear and high-integrity work.)
Built-in error checking + clash detection: Call out the practical outcome: fewer interferences with critical equipment, fewer late redesigns.
Interoperability details engineers care about: Mention bidirectional integration between Aspect Pipe Stress and Aspect Pressure Vessel (analysis) and with Forte 3D / Forte 3DWorx (design). You can also mention the ability to import PCF from many third-party design tools.
Analysis breadth (concrete list): Static + dynamic with modal, response spectrum, harmonic, time history, plus mention load types like thermal, wind/wave, seismic, and support for buried/subsea scenarios (as applicable).
Auxiliary modules:Flange analysis (ASME and EN 1591) and equipment nozzle analysis (multiple standards), plus references like WRC 107/297 and B31G (where available).
Productivity features:Built-in piping wizards, templates for load cases, and report generation in common formats.
Why does it matter for engineers?
Change can be disruptive, but the main practical takeaway is straightforward: CAESAR II is now Octave Aspect Pipe Stress, and the product continues to focus on standards-based pipe stress analysis, reporting, and interoperability with Octave design and analysis tools.
Continuity: If you have existing CAESAR II-based workflows, the rebrand primarily affects product naming and portfolio alignment under Octave.
Workflow efficiency: Aspect Pipe Stress emphasizes integrations with Octave design solutions (including Forte 3D and Forte 3DWorx) to reduce rework and keep design and analysis data aligned.
Model quality: Built-in error checking and clash detection help catch issues early.
Conclusion: The future of pipe stress analysis
Octave Aspect Pipe Stress is the current name for the solution formerly known as CAESAR II. It remains positioned as an industry-leading pipe stress analysis tool with broad code support, robust analysis options, and integrations that help engineering teams deliver safer, more compliant designs.
The latest edition of ASME B31.4-2025 is issued on 31st Dec 2025 by the ASME. This Code will become effective 6 months after the Date of Issuance which means from 1st July 2026 onwards and remain valid till the issuance of the next edition of this code which is scheduled for publication in 2028. The ASME B31.4 Pipeline Transportation Systems for Liquids and Slurries is one of the most important standards in the ASME B31 Pressure Piping Code series. It governs the design, materials, construction, inspection, examination, testing, operation, and maintenance of liquid pipeline systems, including pipelines transporting crude oil, petroleum products, liquid hydrocarbons, anhydrous ammonia, carbon dioxide, and aqueous slurries of nonhazardous materials.
The 2025 edition updates the 2022 version and continues ASME’s effort to align pipeline engineering practices with modern technologies, safety expectations, and regulatory requirements.
This article summarizes the four key changes of the ASME B31.4-2025 edition for pipeline engineers, operators, inspectors, and EPC contractors. Kind request to readers of the article to highlight other major changes that every pipeline engineer should know in the comments section.
1. Inclusion of Sustained Stress Indices (I) for Pipeline Stress Calculation:
For the first time ASME B31.4 includes the application of sustained stress indices (I) for analysis of sustained loads during pipeline stress calculation. The minimum value to be considered for sustained stress indices is 1.0. When more directly applicable data for sustained stress indices are not available, It’s value can be determined in accordance with ASME B31J Table 1-1, General Note (d). However, the designer of the pipeline system is responsible to determine the applicable sustained stress indices if a piping component is not specifically addressed in ASME B31J.
2. Modification of Longitudinal Stress (SL) Equations for Unrestrained Pipe:
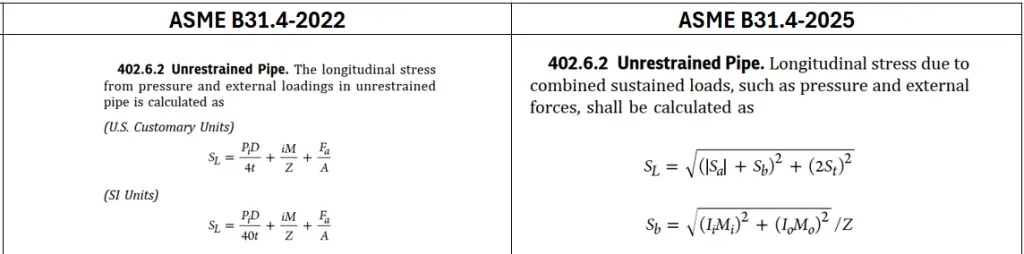
The equations for longitudinal stress (SL) due to sustained loads for unrestrained pipelines are modified entirely. Now the equations approximately matches with the equations provided in ASME B31.3 code. The changes in longitudinal stress equations is given below:
Longitudinal Stress Equation for Unrestrained Pipe as per ASME B31.4
Refer to ASME B31.4, respective editions for the notations and meaning of the terms.
3. Clarifications for Meaning of Suspension of Operation:
The 2025 edition of ASME B31.4 clarifies the meaning and requirements for a pipeline suspension of operation and abandonment. It states,
“Suspending operation of a piping system for any length of time is not considered abandonment. All relevant operation and maintenance procedures shall continue to be applied as if the system were still in service.”
4. Changes in the Calculation of Section Modulus and Cross Sectional Area for Unrestrained Pipe:
ASME B31.4-2025 has updated the calculation of Sustained Section modulus (Z) and Cross Sectional Area (A) with respect to its earlier edition. Now, both the mentioned parameters need to be calculated using nominal pipe dimensions less allowances. Till 2022 edition of ASME B31.4, all these calculations were based on nominal pipe thicknesses.
So, ASME B31.4-2025 made the longitudinal stress calculation for unrestrained liquid and slurry pipelines more conservative and stress engineers will find more difficulty in its qualification.
Also, the unit system (US system or SI system) specific equations are now removed and ASME B31.4, 2025 edition provides one single equation for each variables in both units.
These are the four major changes that are known to us till date. If you come across any other changes please mention the same in the comments section and we will add those in due course.